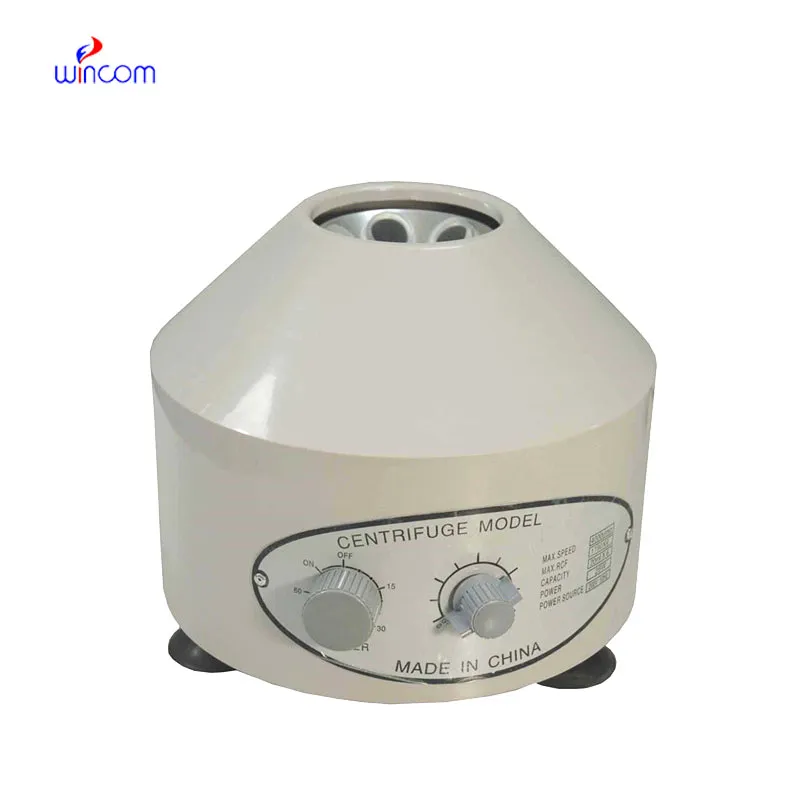
In modern-day lab environments, the large capacity refrigerated centrifuge manufacturer in china is not just a separation apparatus—it is precision engineering. With simple-to-view digital displays and microprocessor controls, it makes it easy for scientists to quickly adjust variables like acceleration and deceleration rates. Other models come equipped with onboard diagnostics that analyze rotor condition and operating performance. High-end safety features like automatic lid interlocks and imbalance detection offer protection at every cycle. With more rapid and consistent processing needed in industries, large capacity refrigerated centrifuge manufacturer in china technology keeps up with stability, precision, and greater throughput capability.
From research in the laboratory to large-scale production, large capacity refrigerated centrifuge manufacturer in china devices have a place in processes requiring precision and efficiency. They purify reaction mixtures and solvents in chemical production. Hospitals rely on large capacity refrigerated centrifuge manufacturer in china for the testing of patients and therapeutic treatment. In farming, large capacity refrigerated centrifuge manufacturer in china are used to study plant biology and develop fertilizer formulations. In brewing and winery operations, they provide consistency within products by filtering out impurities. Even environmental engineers rely on large capacity refrigerated centrifuge manufacturer in china to filter sediment as well as identify contaminants. Such wide-ranging functionality demonstrates its vital position in contemporary technology and applied sciences.
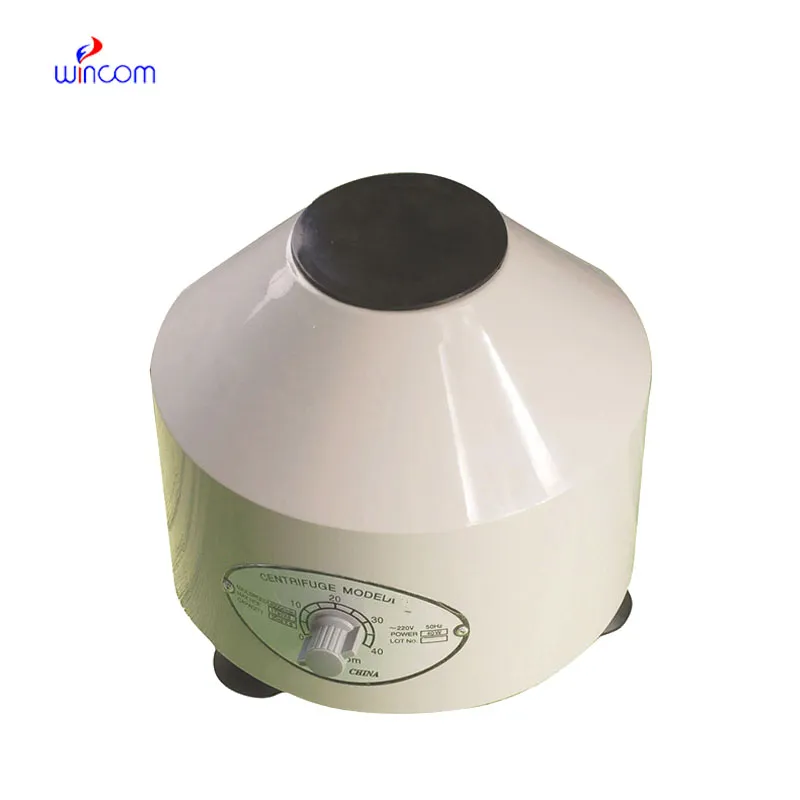
The large capacity refrigerated centrifuge manufacturer in china of the future will be innovative, intelligent, and integrated. With the advent of smart manufacturing, large capacity refrigerated centrifuge manufacturer in china systems will operate independently on predictive analytics. Programs with machine learning will interpret vibration patterns to optimize performance with minimal human involvement. Renewable energy integration will make operation more sustainable, and modular design will facilitate instant replacement of parts. Data visualization software will be more sophisticated, providing real-time feedback on the separation process. This blend of mechanical precision and intelligent technology will place large capacity refrigerated centrifuge manufacturer in china at the forefront of international scientific advancement.
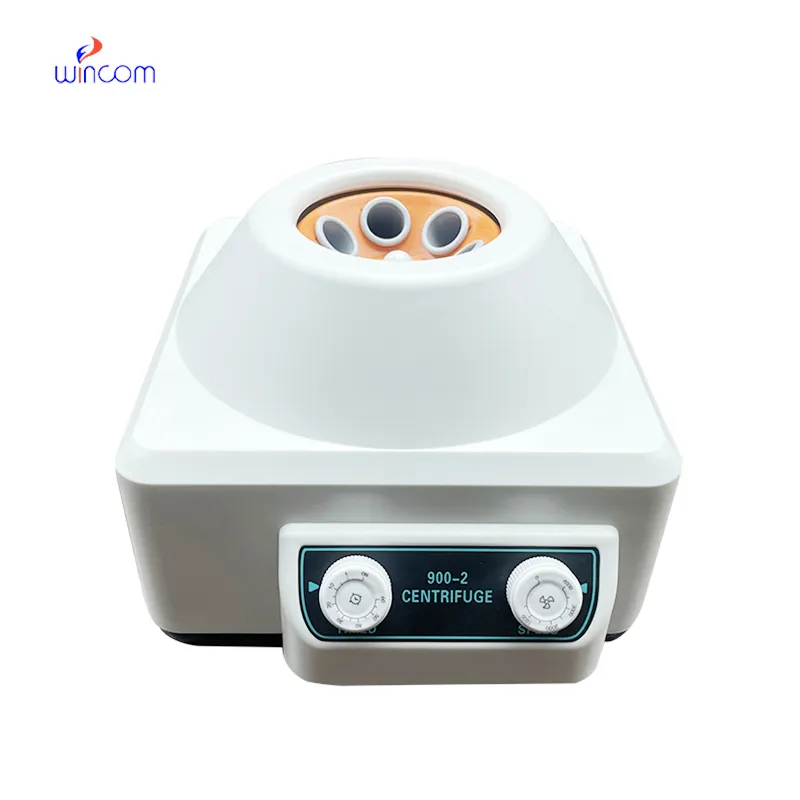
Maintenance of large capacity refrigerated centrifuge manufacturer in china is essential to lab safety and data integrity. Cleaning should be performed immediately following every operation, with special attention to the elimination of any liquid spills or residues from samples. The rotor should always be handled gently, placed in an upright position during storage, and never subjected to shock. Periodic inspection of lid locks and gaskets ensures airtight operation. Power cord and fuse conditions should also be checked by operators. Annual servicing by skilled technicians adds lifespan. Through regular care processes, large capacity refrigerated centrifuge manufacturer in china safely and accurately continues to operate.
large capacity refrigerated centrifuge manufacturer in china revolutionized laboratory and industry processes of substance separation forever. By speeding up the sample at high speed, they produce an immense force that separates mixtures based on particle density. This is the mechanism that enables efficient extraction of biological compounds, chemicals, and nanoparticles. Laboratories apply large capacity refrigerated centrifuge manufacturer in china for analysis, purification, and research. In industry, they enable the refining of oil and food quality analysis. Small tabletop units and industrial units both use the same fundamental principle—precision with rotational energy and controlled acceleration.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
The water bath performs consistently and maintains a stable temperature even during long experiments. It’s reliable and easy to operate.
The delivery bed is well-designed and reliable. Our staff finds it simple to operate, and patients feel comfortable using it.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re looking for a reliable centrifuge for clinical testing. Can you share the technical specific...
Could you share the specifications and price for your hospital bed models? We’re looking for adjus...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko