In modern-day lab environments, the large capacity refrigerated centrifuge manufacturer is not just a separation apparatus—it is precision engineering. With simple-to-view digital displays and microprocessor controls, it makes it easy for scientists to quickly adjust variables like acceleration and deceleration rates. Other models come equipped with onboard diagnostics that analyze rotor condition and operating performance. High-end safety features like automatic lid interlocks and imbalance detection offer protection at every cycle. With more rapid and consistent processing needed in industries, large capacity refrigerated centrifuge manufacturer technology keeps up with stability, precision, and greater throughput capability.
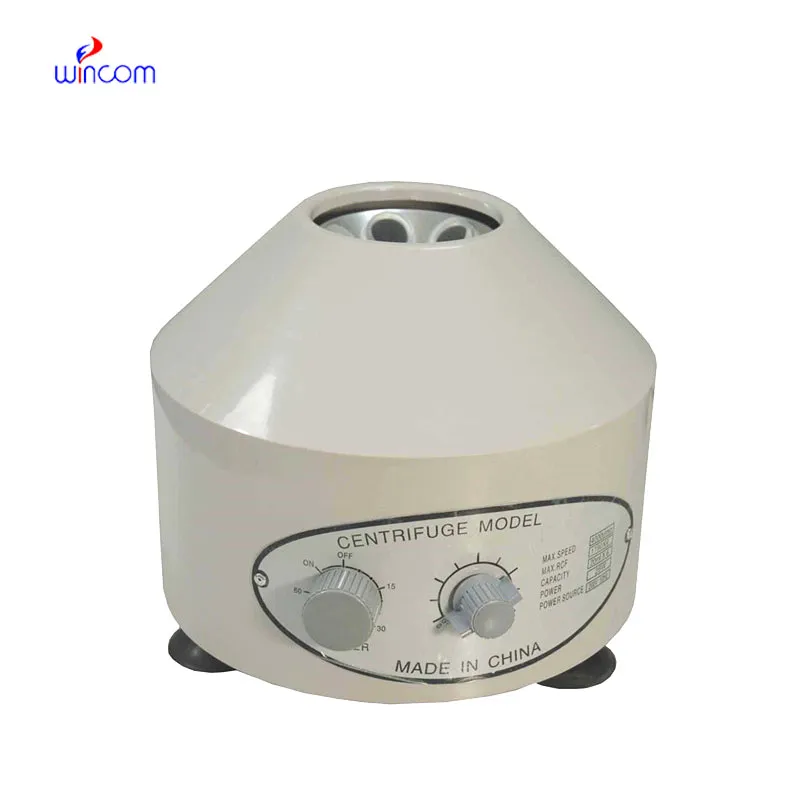
Clinical laboratory environments utilize large capacity refrigerated centrifuge manufacturer as an important tool for proper diagnosis. Blood banks utilize it to efficiently isolate red cells, plasma, and platelets. Research laboratories employ large capacity refrigerated centrifuge manufacturer to examine tissue samples for cellular and molecular studies. In the energy industry, it assists in the manufacture of biofuels by isolating the biomass components. Food scientists employ large capacity refrigerated centrifuge manufacturer to reclaim fats and purify proteins while preparing products. The numerous applications reflect its capacity to enhance data reliability, process control, and yield output in a wide variety of industries and research applications.
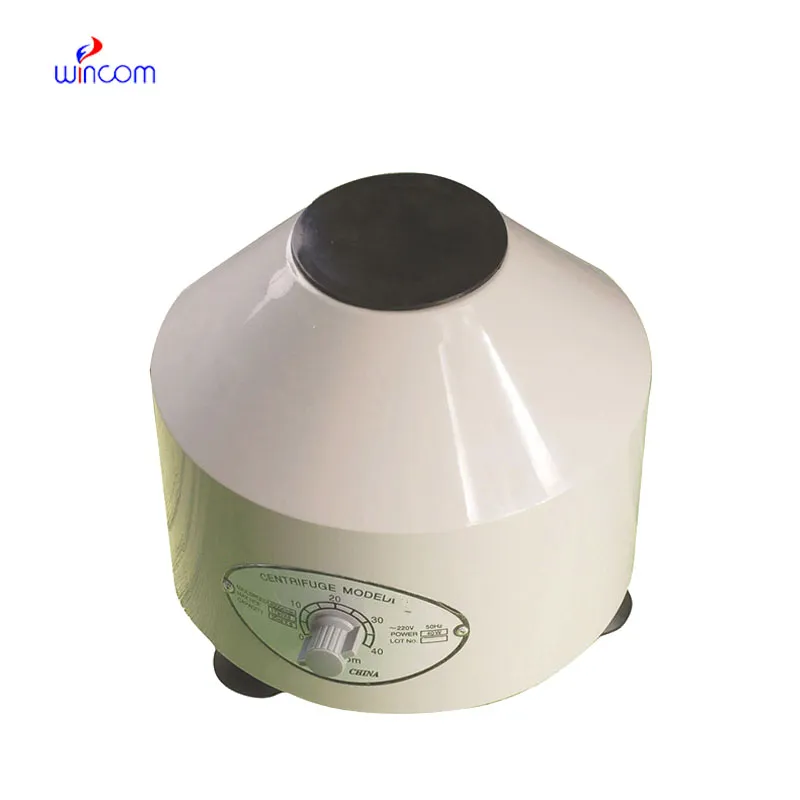
{Keywords} of the future will unprecedentedly advance in performance and design. Future systems will feature adaptive balancing technology that adjusts to dynamic loads in real time. Intelligent rotors will track stress and fatigue in real time, allowing for extended service life. With IoT connectivity, multiple large capacity refrigerated centrifuge manufacturer units will be remotely managed to streamline laboratory networks. In biomedical applications, miniaturized devices will facilitate high-throughput screening with low sample volumes. These advancements are a step toward smarter, faster, and greener devices that revolutionize how separation processes are controlled in modern science.
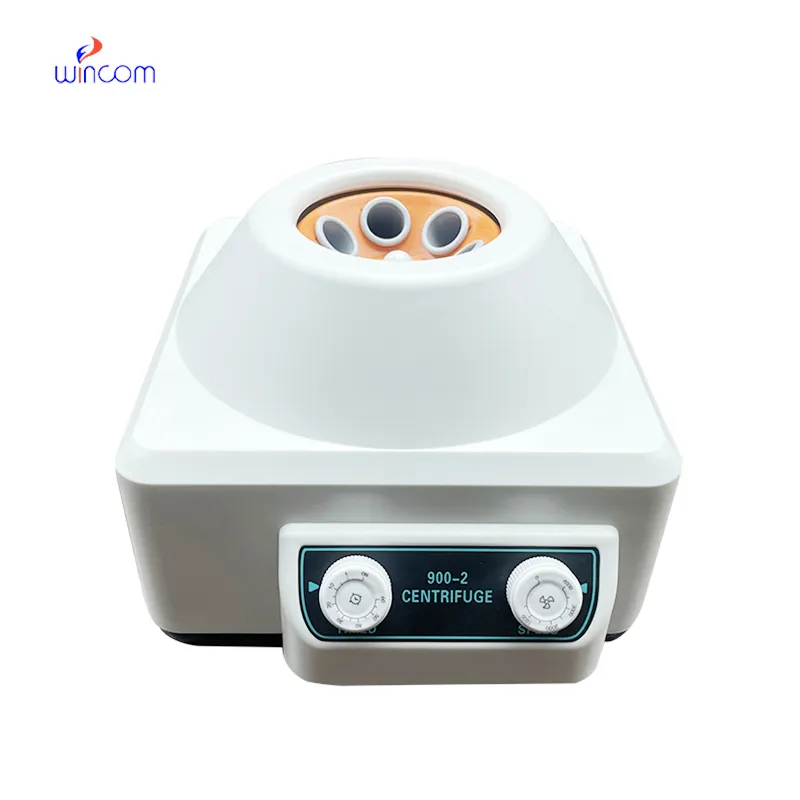
For optimal performance, large capacity refrigerated centrifuge manufacturer equipment needs to be handled cautiously and carefully. Operators need to ensure that rotors are balanced before use to avert vibration and wear. Regular cleaning of inner and outer surfaces prevents residues from building up that can impact results. Electric wiring should be inspected for loose or damaged cables. Storage of large capacity refrigerated centrifuge manufacturer in a clean, temperature-controlled environment keeps its components. Regular professional maintenance and replacement of worn parts on schedule ensure smooth and efficient use of the device over time.
Through controlled rotation, a large capacity refrigerated centrifuge manufacturer produces very high outward pressure that separates the components of a mixture. It is used comprehensively in medical diagnosis, chemical analysis, and materials science. Its efficacy lies in uniform velocity and balance, producing neat separation of liquids and solids. Most large capacity refrigerated centrifuge manufacturer today have digital timers, automatic lid closing, and temperature regulation. Such the inclusion of safety and efficiency has made the large capacity refrigerated centrifuge manufacturer a staple of modern research and manufacturing, providing faster and more accurate results across industries.
Q: What factors affect the performance of a centrifuge? A: Performance depends on rotor design, speed accuracy, load balance, and regular maintenance of mechanical and electrical parts. Q: How should a centrifuge be cleaned? A: Use a soft cloth and mild detergent to clean the chamber and rotor, avoiding abrasive or corrosive substances that could cause damage. Q: Can a centrifuge be used for temperature-sensitive samples? A: Yes, refrigerated models are designed to maintain stable temperatures, protecting samples from heat generated during rotation. Q: What does RPM mean in centrifuge operation? A: RPM stands for revolutions per minute, indicating how fast the rotor spins—higher RPMs generate stronger centrifugal forces. Q: When should the rotor of a centrifuge be replaced? A: Rotors should be replaced when signs of fatigue, corrosion, or cracking appear, or after reaching the manufacturer’s specified lifespan.
The hospital bed is well-designed and very practical. Patients find it comfortable, and nurses appreciate how simple it is to operate.
The delivery bed is well-designed and reliable. Our staff finds it simple to operate, and patients feel comfortable using it.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We are planning to upgrade our imaging department and would like more information on your mri machin...
Hello, I’m interested in your water bath for laboratory applications. Can you confirm the temperat...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko